2 little Indians
- Klipkopwildlife
-
 Topic Author
- Offline
- Administrator
-

- I'm supposed to be retired!
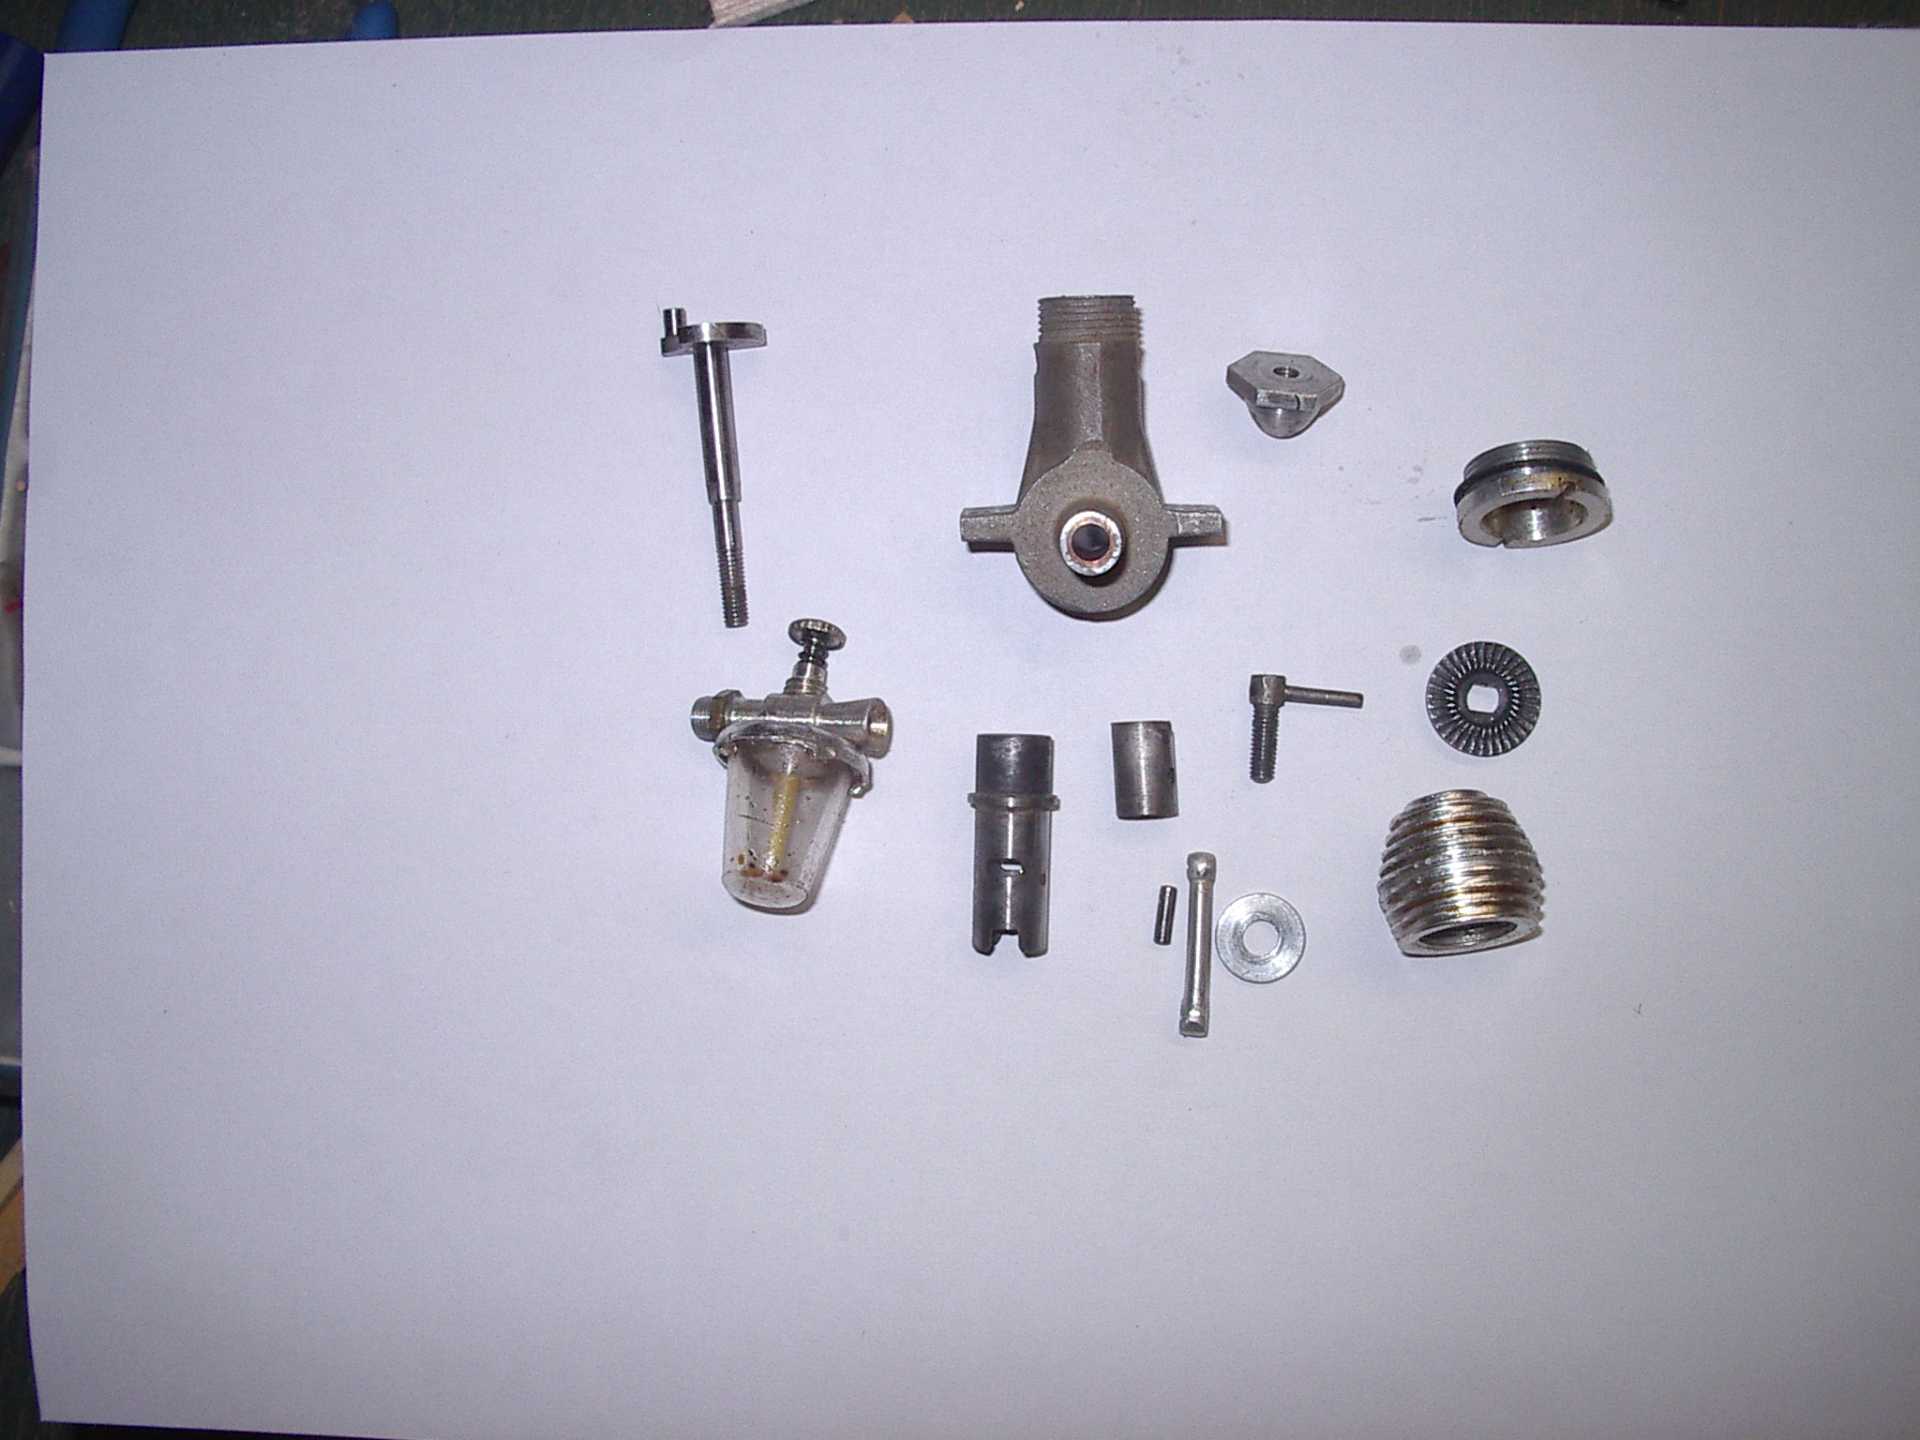
I've finally got the cylinder out without damage, yes, firmly glued in with old Castor oil!
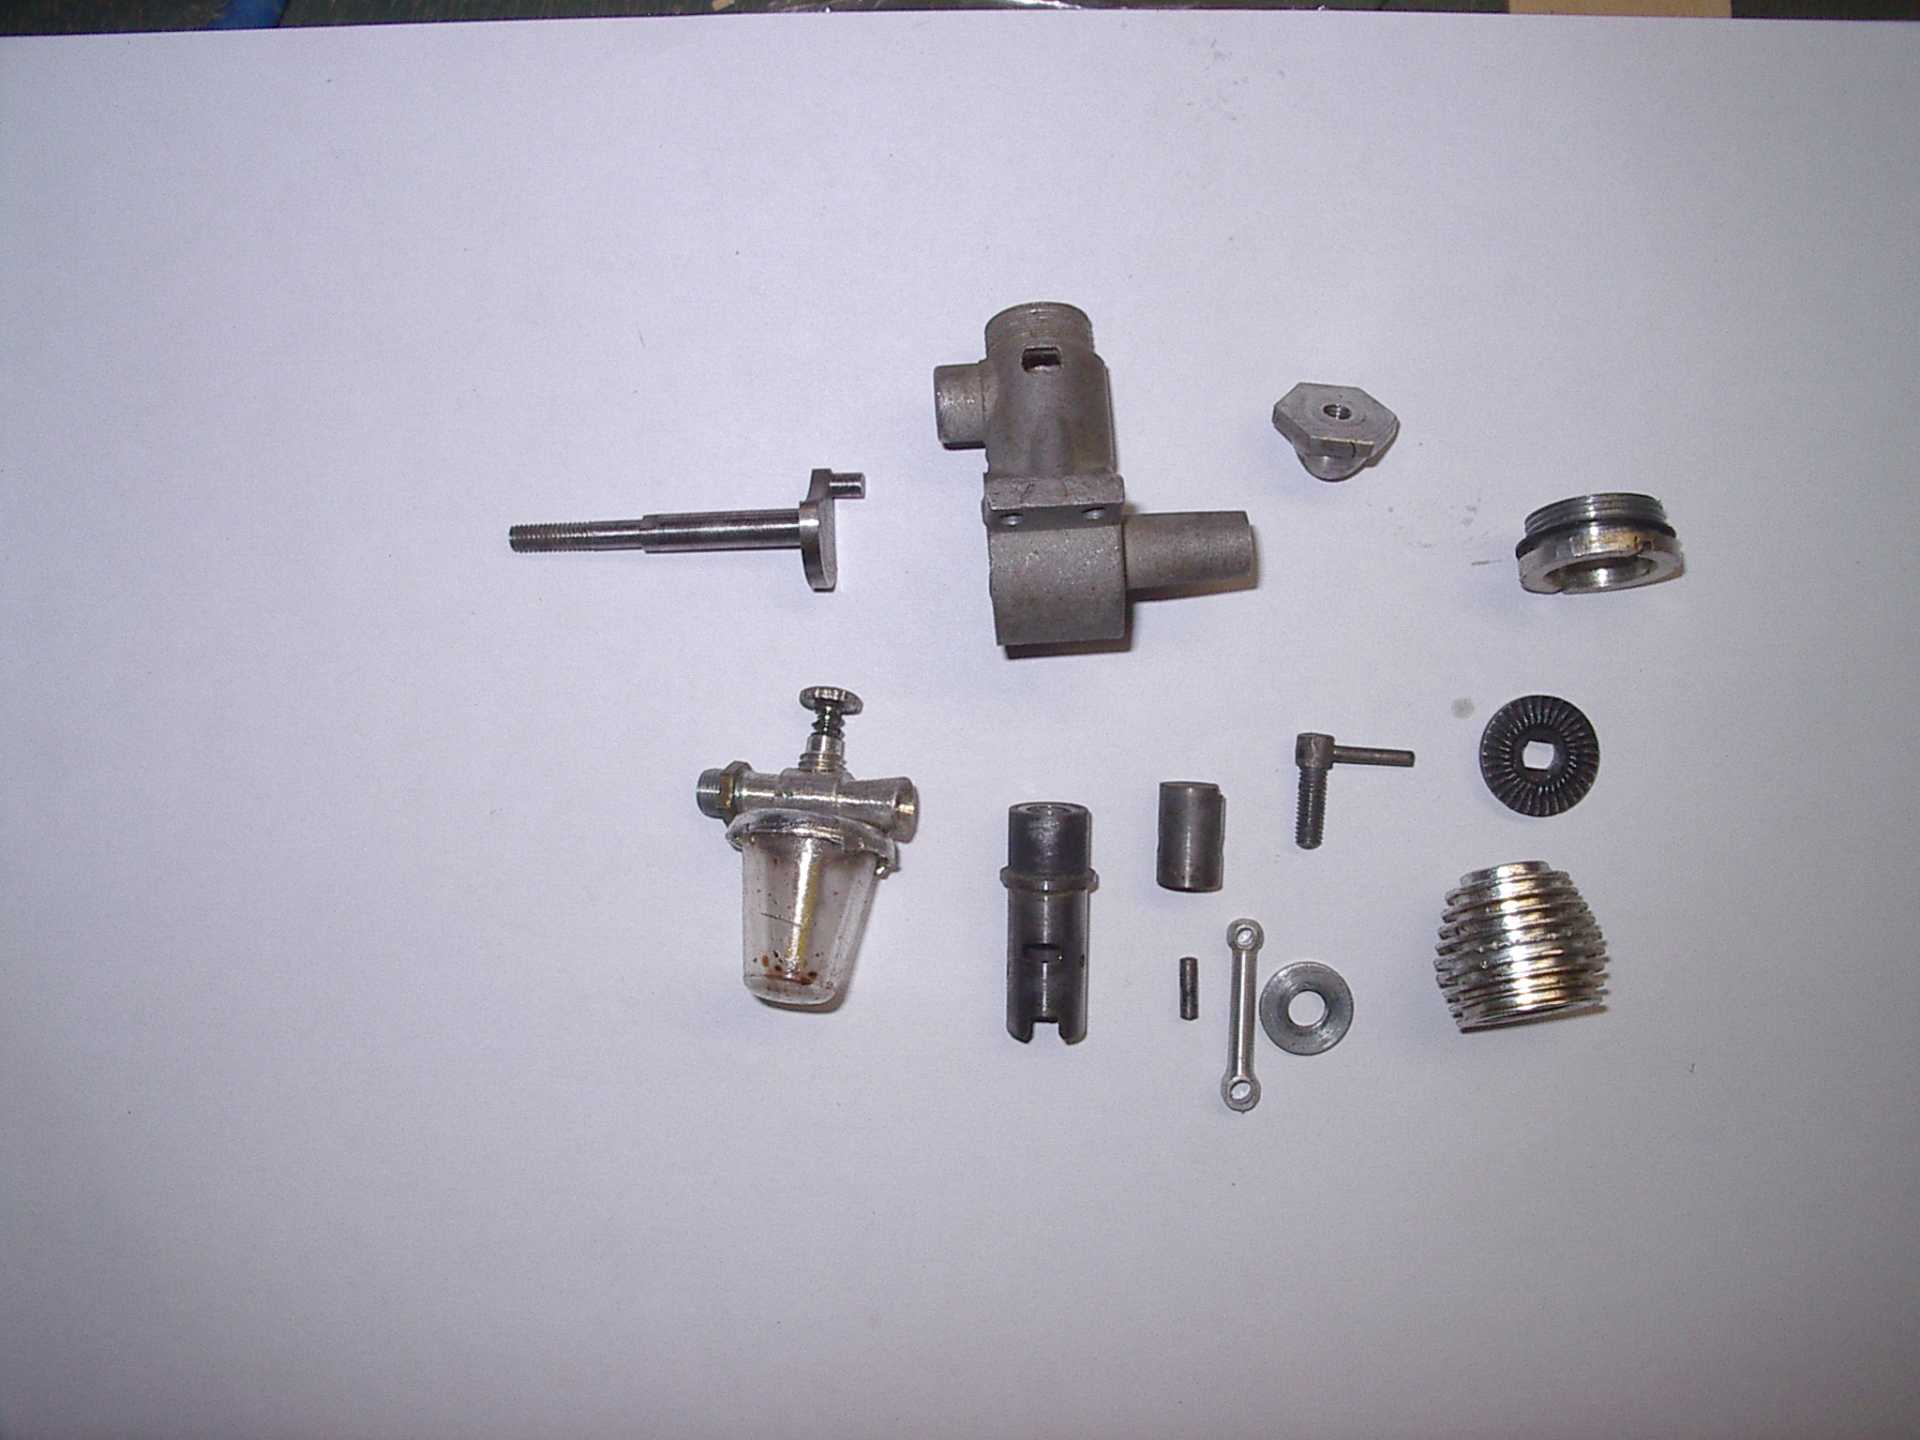
This engine has had very little use, I'm guessing just a proving run and then put away for years.
Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.
- Klipkopwildlife
-
Topic Author
- Offline
- Administrator
-
- I'm supposed to be retired!

The connecting rod is bent!

Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.
- Klipkopwildlife
-
Topic Author
- Offline
- Administrator
-
- I'm supposed to be retired!
Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.
- Quorneng
-

- Offline
- Forum Master
-

- Posts: 9436
- Thank you received: 19043
More important than perfectly flat is that the big and little end bearings are parallel to each other.

Please Log in or Create an account to join the conversation.
- Klipkopwildlife
-
Topic Author
- Offline
- Administrator
-
- I'm supposed to be retired!
So, as you suggest Simon I have to straighten the rod.
To put things in perspective here, a hair from my head (I have very fine hair) measures 0.06mm or .002" (2 thousandths of an inch) and yet the difference renders the component unusable!
Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.
- Klipkopwildlife
-
Topic Author
- Offline
- Administrator
-
- I'm supposed to be retired!

You will remember I noticed file marks on the nose of #1, a glance at the pic shows that #1s' nose is actually shorter and worse, not even square! The measured difference is 1.5mm (1/16" Garry)
Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.
- THE BLACKBIRD
-

- Offline
- Forum Master
-
- Posts: 6368
- Thank you received: 10842
Please Log in or Create an account to join the conversation.
- Quorneng
-
- Offline
- Forum Master
-
- Posts: 9436
- Thank you received: 19043
Please Log in or Create an account to join the conversation.
- Klipkopwildlife
-
Topic Author
- Offline
- Administrator
-
- I'm supposed to be retired!
I thought I'd start on the new prop washer today.

3mm Gauge plate

A cut square, oversize, with 3.5mm hole.
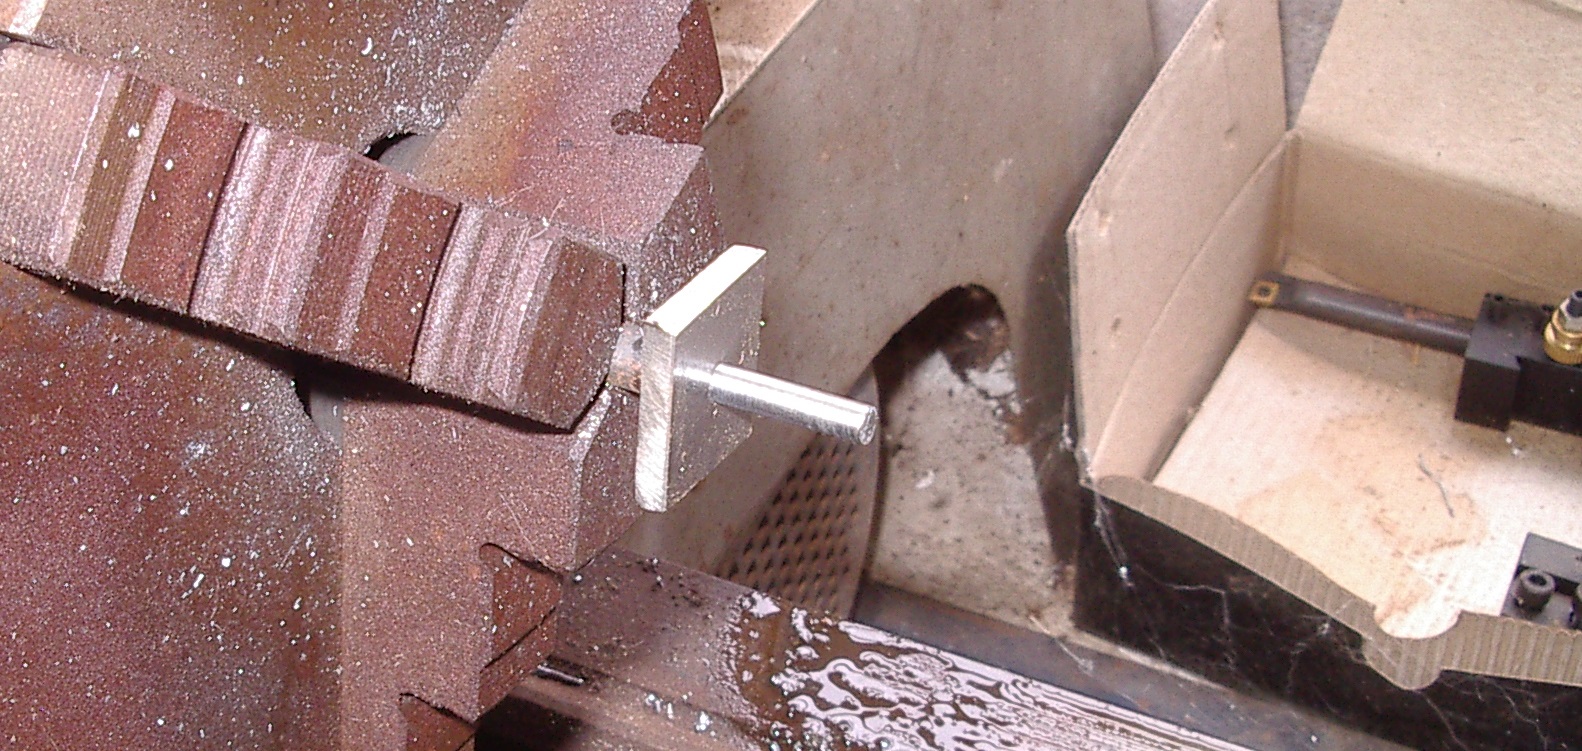
Dummy shaft turned and fit tested.
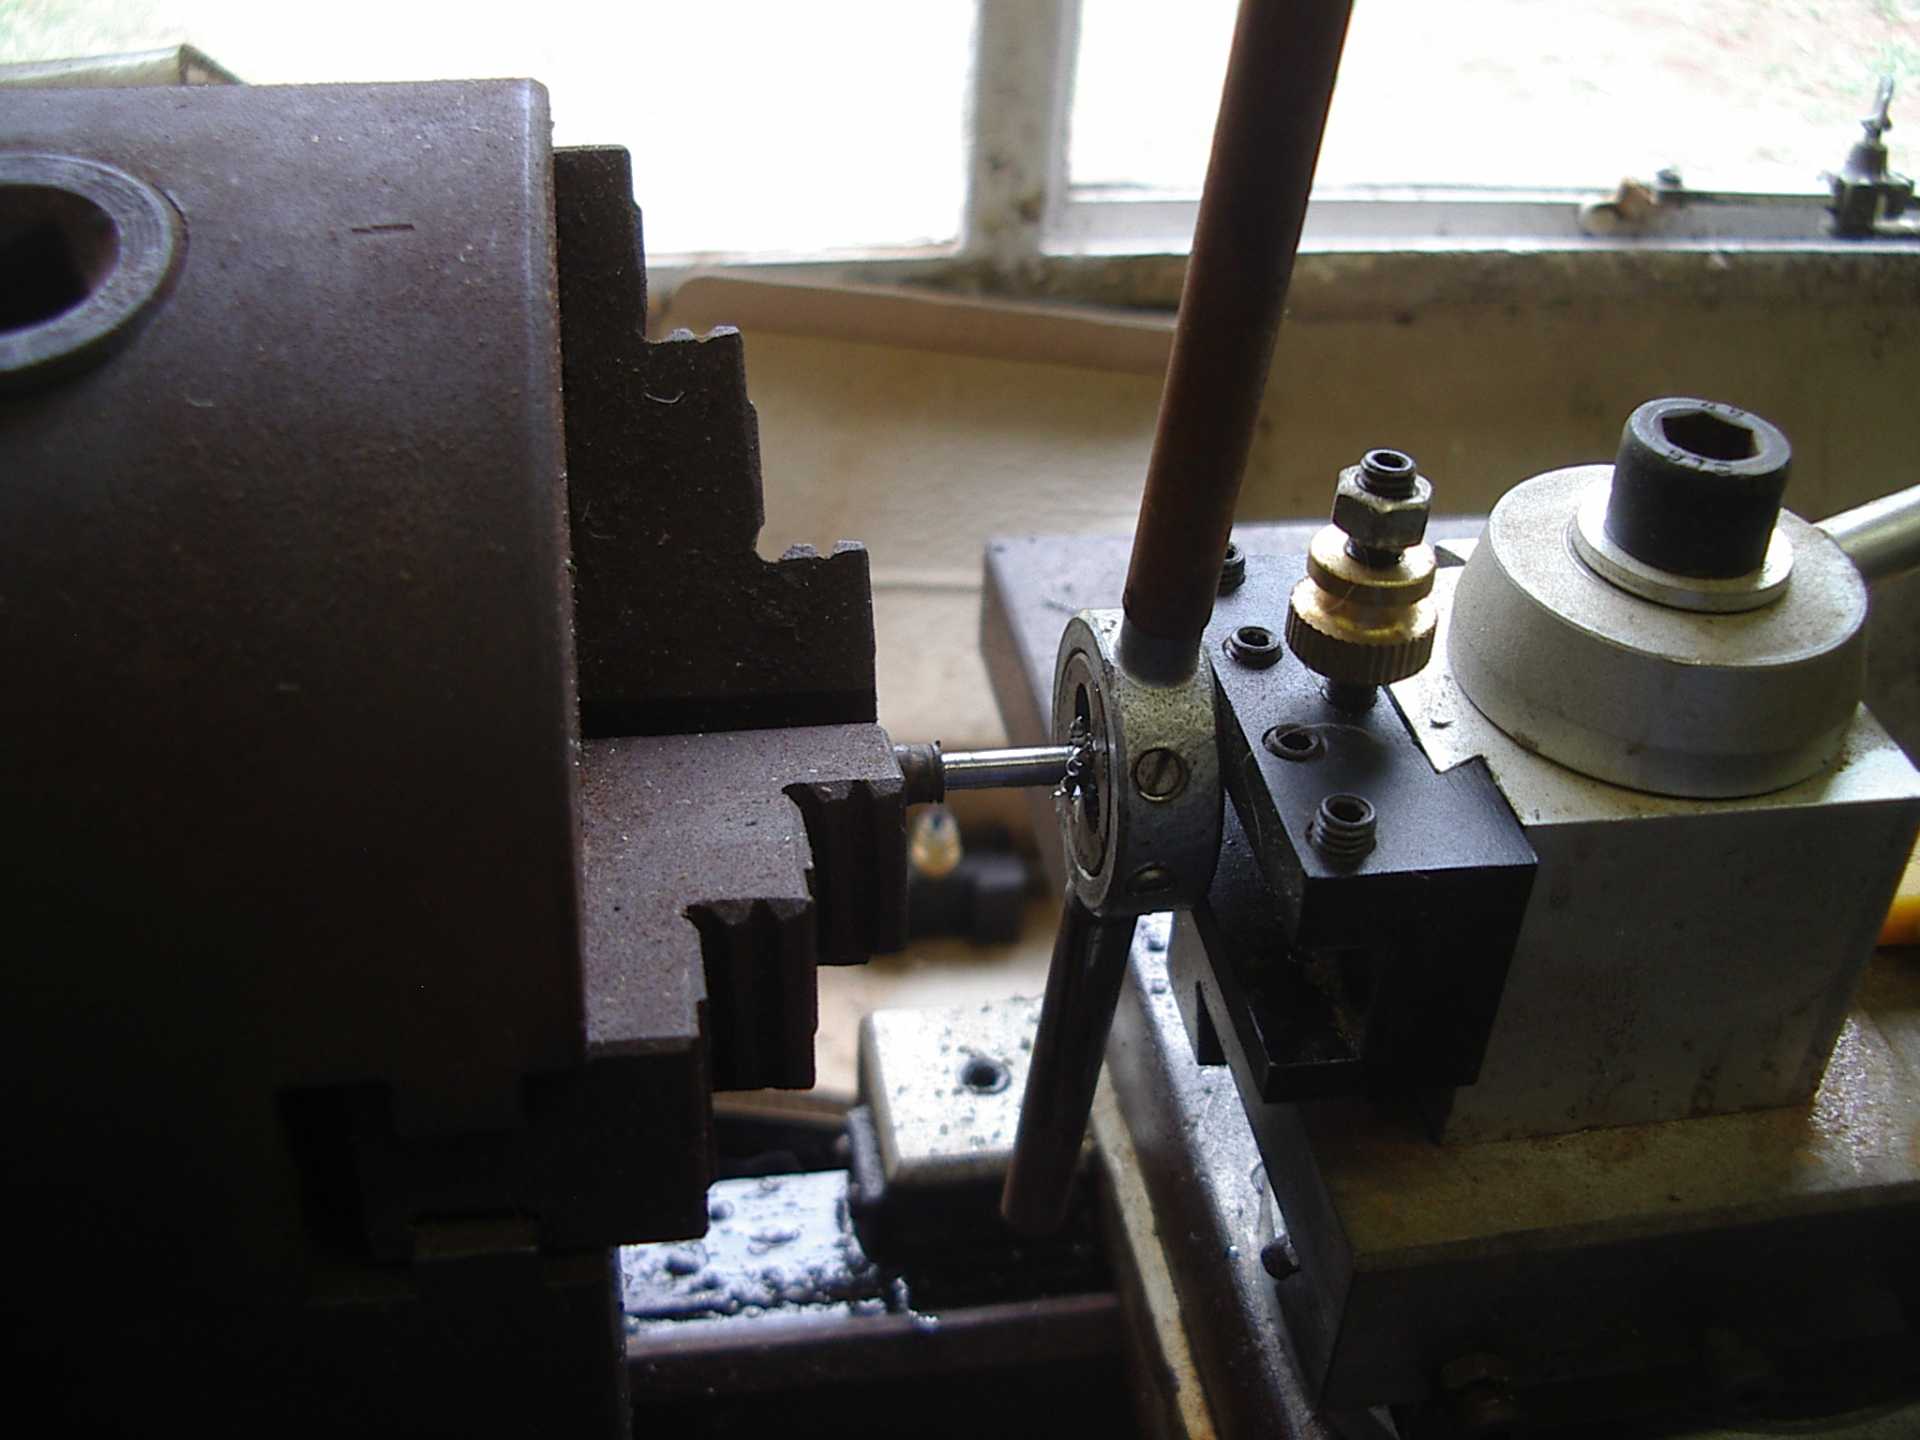
4BA thread going on.
Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.
- boz
-

- Offline
- Platinum Member
-

- Posts: 1176
- Thank you received: 1420
Please Log in or Create an account to join the conversation.
- Quorneng
-
- Offline
- Forum Master
-
- Posts: 9436
- Thank you received: 19043
That 3 jaw has an interesting....er.....finish on it! :woohoo:
Please Log in or Create an account to join the conversation.
- Squirrelnet
- Offline
- Elite Member
-

- Posts: 754
- Thank you received: 2067
Please Log in or Create an account to join the conversation.
- Klipkopwildlife
-
Topic Author
- Offline
- Administrator
-
- I'm supposed to be retired!
At altitude with a clear sky the temperature can drop quite low at dawn. The instant the sun is fully above the horizon warm moist air moves in and everything, especially metal, which holds the coolth, gets soaking wet! I try and keep things oiled up but it doesn't always happen. Even things kept in drawers gets a fine patina of rust very quickly.Quorneng wrote: Very nice Klippy.
That 3 jaw has an interesting....er.....finish on it! :woohoo:
Well I've done some more

And turned to the finish od.

Job done, milling next.
This old girl is very aggressive when she's got kids and terrorises the dogs!
Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.
- Klipkopwildlife
-
Topic Author
- Offline
- Administrator
-
- I'm supposed to be retired!

Turned down to be a tight fit in the crankshaft bearing.

Mounted up

And finished. I had to take 1.2mm off to true it up! If you look very closely you can see casting metal intruding into the bronze bearing. I'm pretty sure these crankcases were cast around the bronze bearing which was then reamed to size.
Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.
- Klipkopwildlife
-
Topic Author
- Offline
- Administrator
-
- I'm supposed to be retired!

My boring bar is a little large for this job but I've skimmed the rear of the engine mounts to give a flat surface. Just a feasibility study on this engine. The carburettor attachment boss gets in the way but enough of the mounts can be machined to give a true surface. What showed up here was that the facing and threading of the rear case is way off centre and out of true!
The moulds for the pressure die casting machine are obviously badly worn which means machining the rear is out of true for the jig they had.
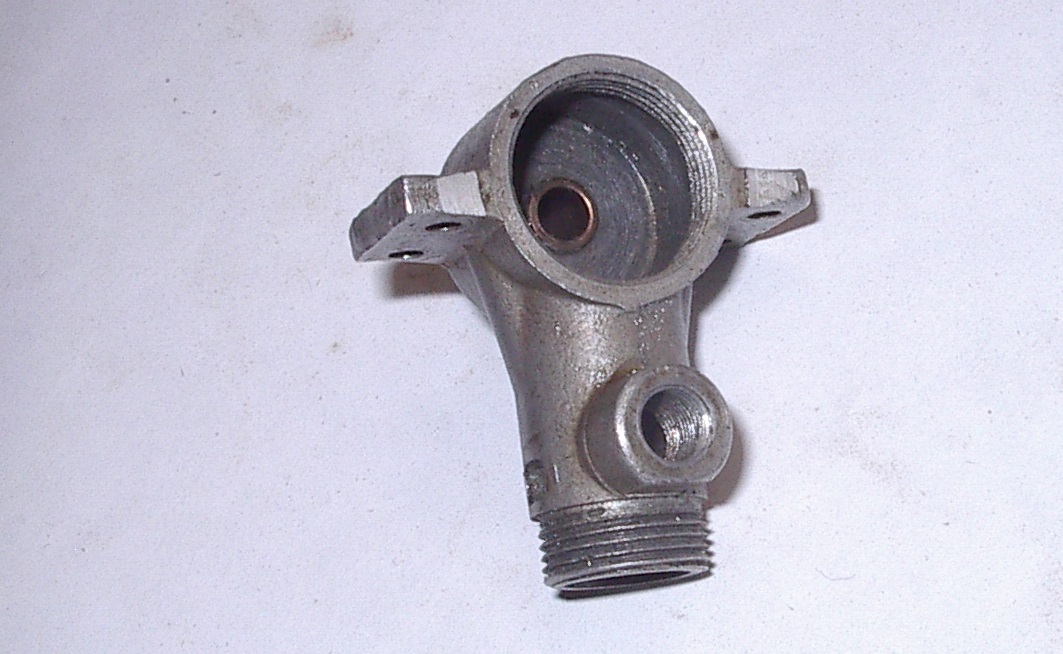
Since this was only a feasibility study I only went far enough to touch both sides. What showed up is that the turned and threaded rear of the crankcase is .3mm out of true with the crankshaft.
Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.