JB Atoms
- Klipkopwildlife
-
 Topic Author
- Offline
- Administrator
-

- I'm supposed to be retired!
Thanks Doug, Mr Burford is a man after my own heart and has me drooling over some (all?) of the machines he has!Doug wrote: I believe Mills engines used hardened pistons and cylinder, and because of this were virtually impossible to wear out. A modern example of this set up is the very high quality Peter Burford 0.3cc engine. This explanation on his web site states that a small variation in hardness is enough to prevent galling. See www.peterburford.com.au/construction/
Doug
Certainly the Indian Mills have not been hardened anywhere!
Boz, General engineering practice is that Ball races can be hard outer, hard balls and hard inner because there is no slippage between surfaces. (Paradoxically using too good a grease (Molybdenum disulphide for example) encourages slide, leading to the rapid demise of the race)
Where you have two surfaces with differing speeds it is normal in the motor industry to fit a dissimilar material as a carrier, bronze or white metal are examples. The thinking is that the softer material picks up any impurities in the oil, these impurities (grit etc) could cause galling elsewhere in the machine.
As Mr Burford says, a difference of 7 Rockwell hardness's is enough to stop galling (pick up) and I still don't like the idea of running steel on steel!
Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.
- Quorneng
-

- Offline
- Forum Master
-

- Posts: 10058
- Thank you received: 19043
Steel piston rings with steel liners. Just sliding and pretty common.

Please Log in or Create an account to join the conversation.
- Klipkopwildlife
-
Topic Author
- Offline
- Administrator
-
- I'm supposed to be retired!
The piston ring/cylinder example is cheating a bit, the ring is very hard (try expanding one too far some time) and the cylinder is very soft (relatively speaking) otherwise you would never be able to re-bore. Mr Burfords' 7 points of Rockwell would appear to hold true. The problem with testing for Rockwell hardness is that the test damages the part, and I don't have the facilities.
To continue

This is the EN30B ready to turn, why is it coloured you ask? All types of steel have an international colour code, normally painted on the end of the bar stock. Once the bar stock end has been cut off it becomes the Storemans job to paint the code down the entire length of bar!
Most damage in factories is caused by incorrect steels being fed into the system!

Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.
- Klipkopwildlife
-
Topic Author
- Offline
- Administrator
-
- I'm supposed to be retired!

Here I've doubled the feed rate in an attempt to get the chip to break. This is a cheap Chinese machine, the spindle speed has dropped and the chip is no longer curling, answer, more horse power, I don't have any.
 (It's 1.5Hp, belt drive)
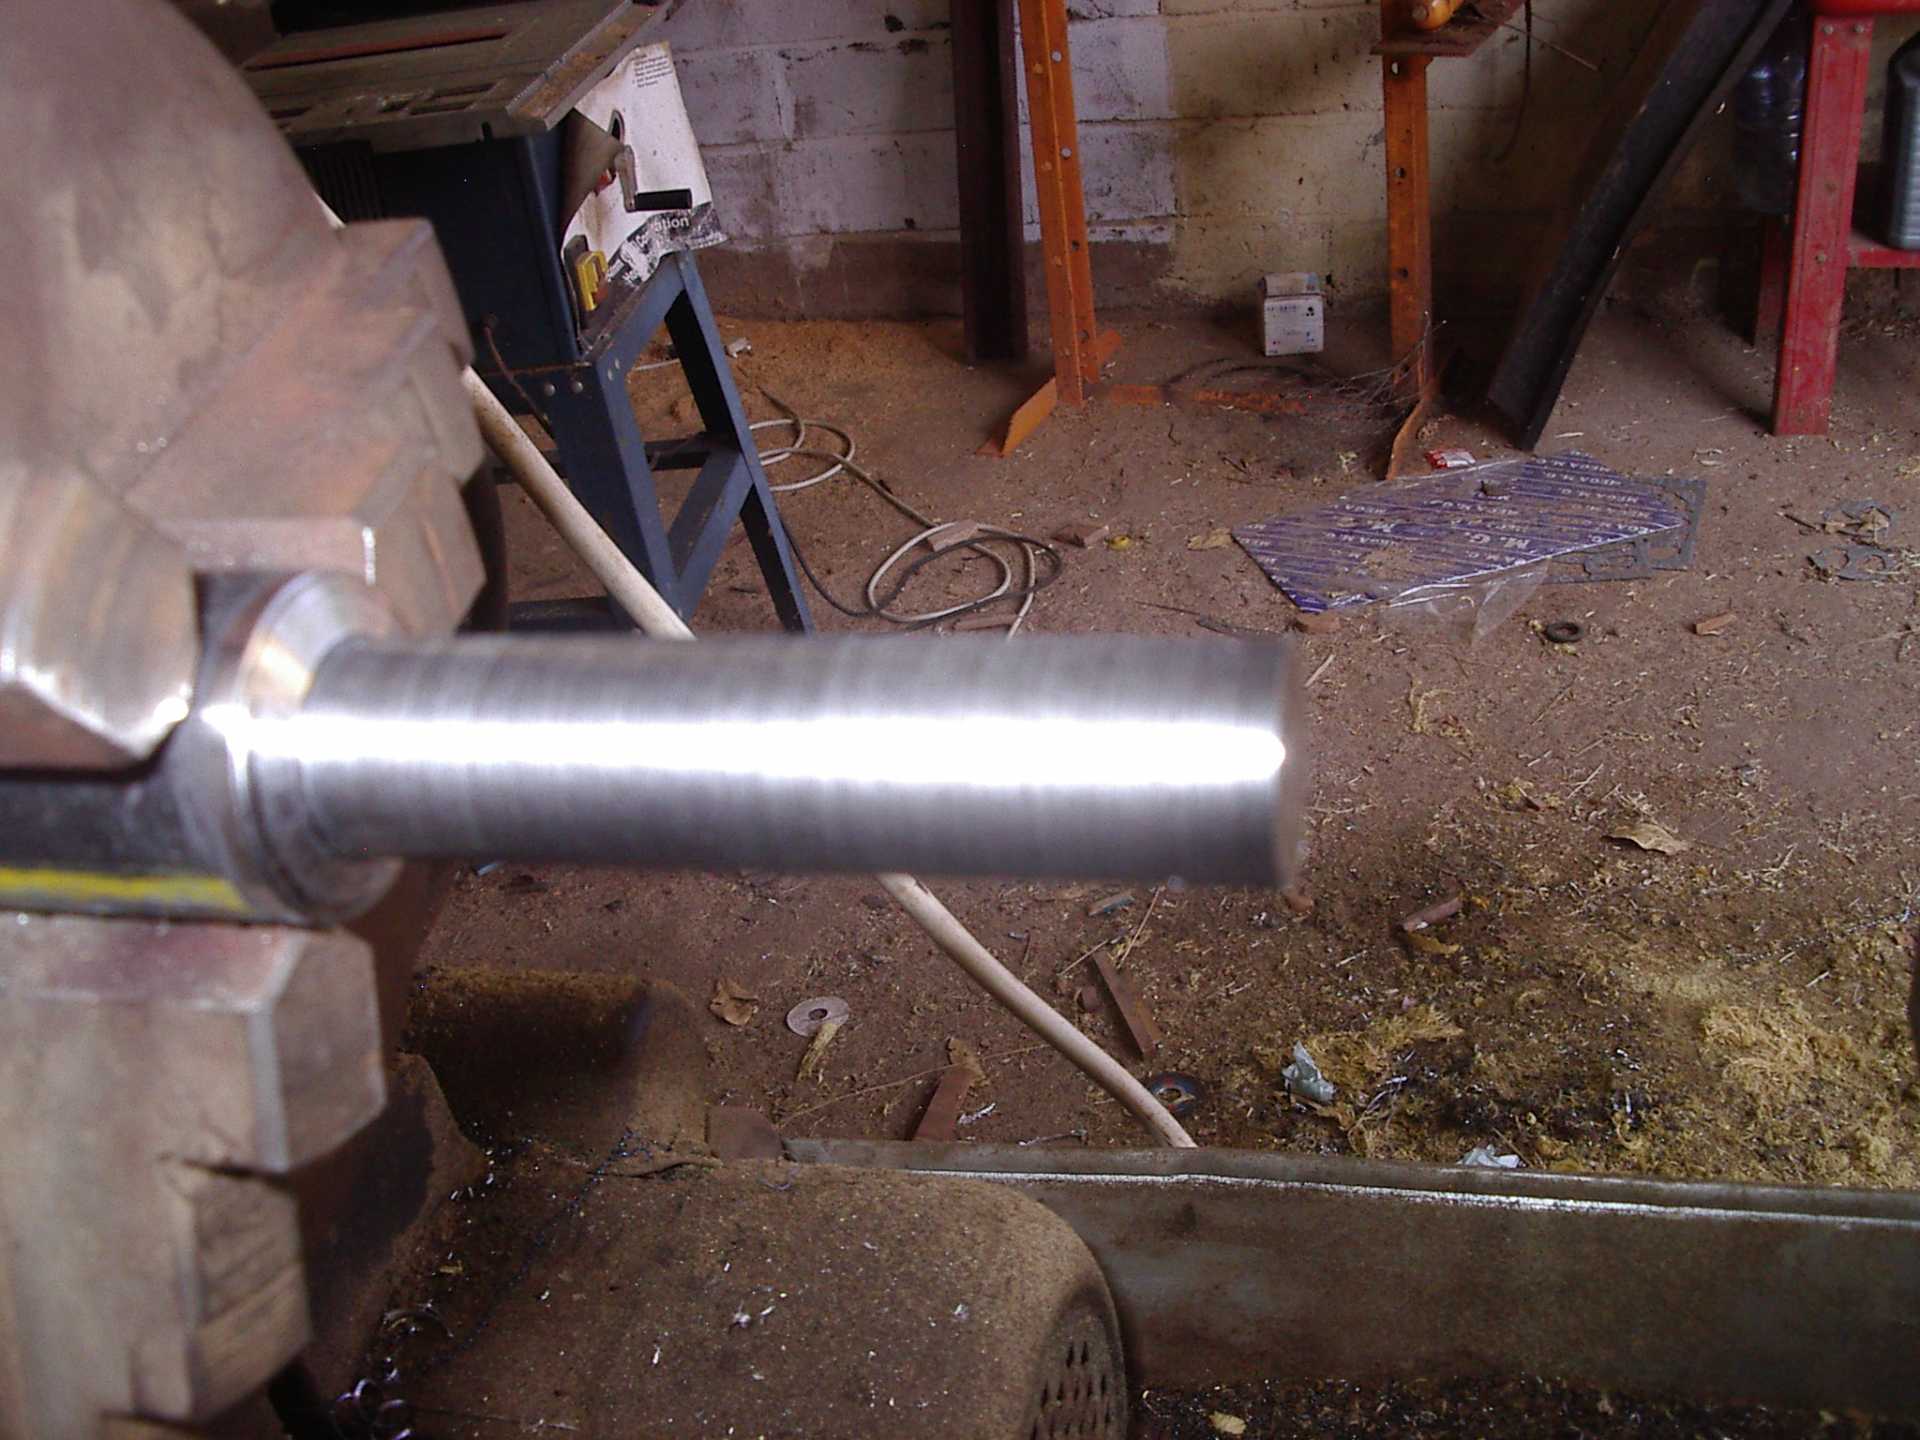
The material turned down the the outside diameter of the crank web, our first objective.
Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.
- Klipkopwildlife
-
Topic Author
- Offline
- Administrator
-
- I'm supposed to be retired!
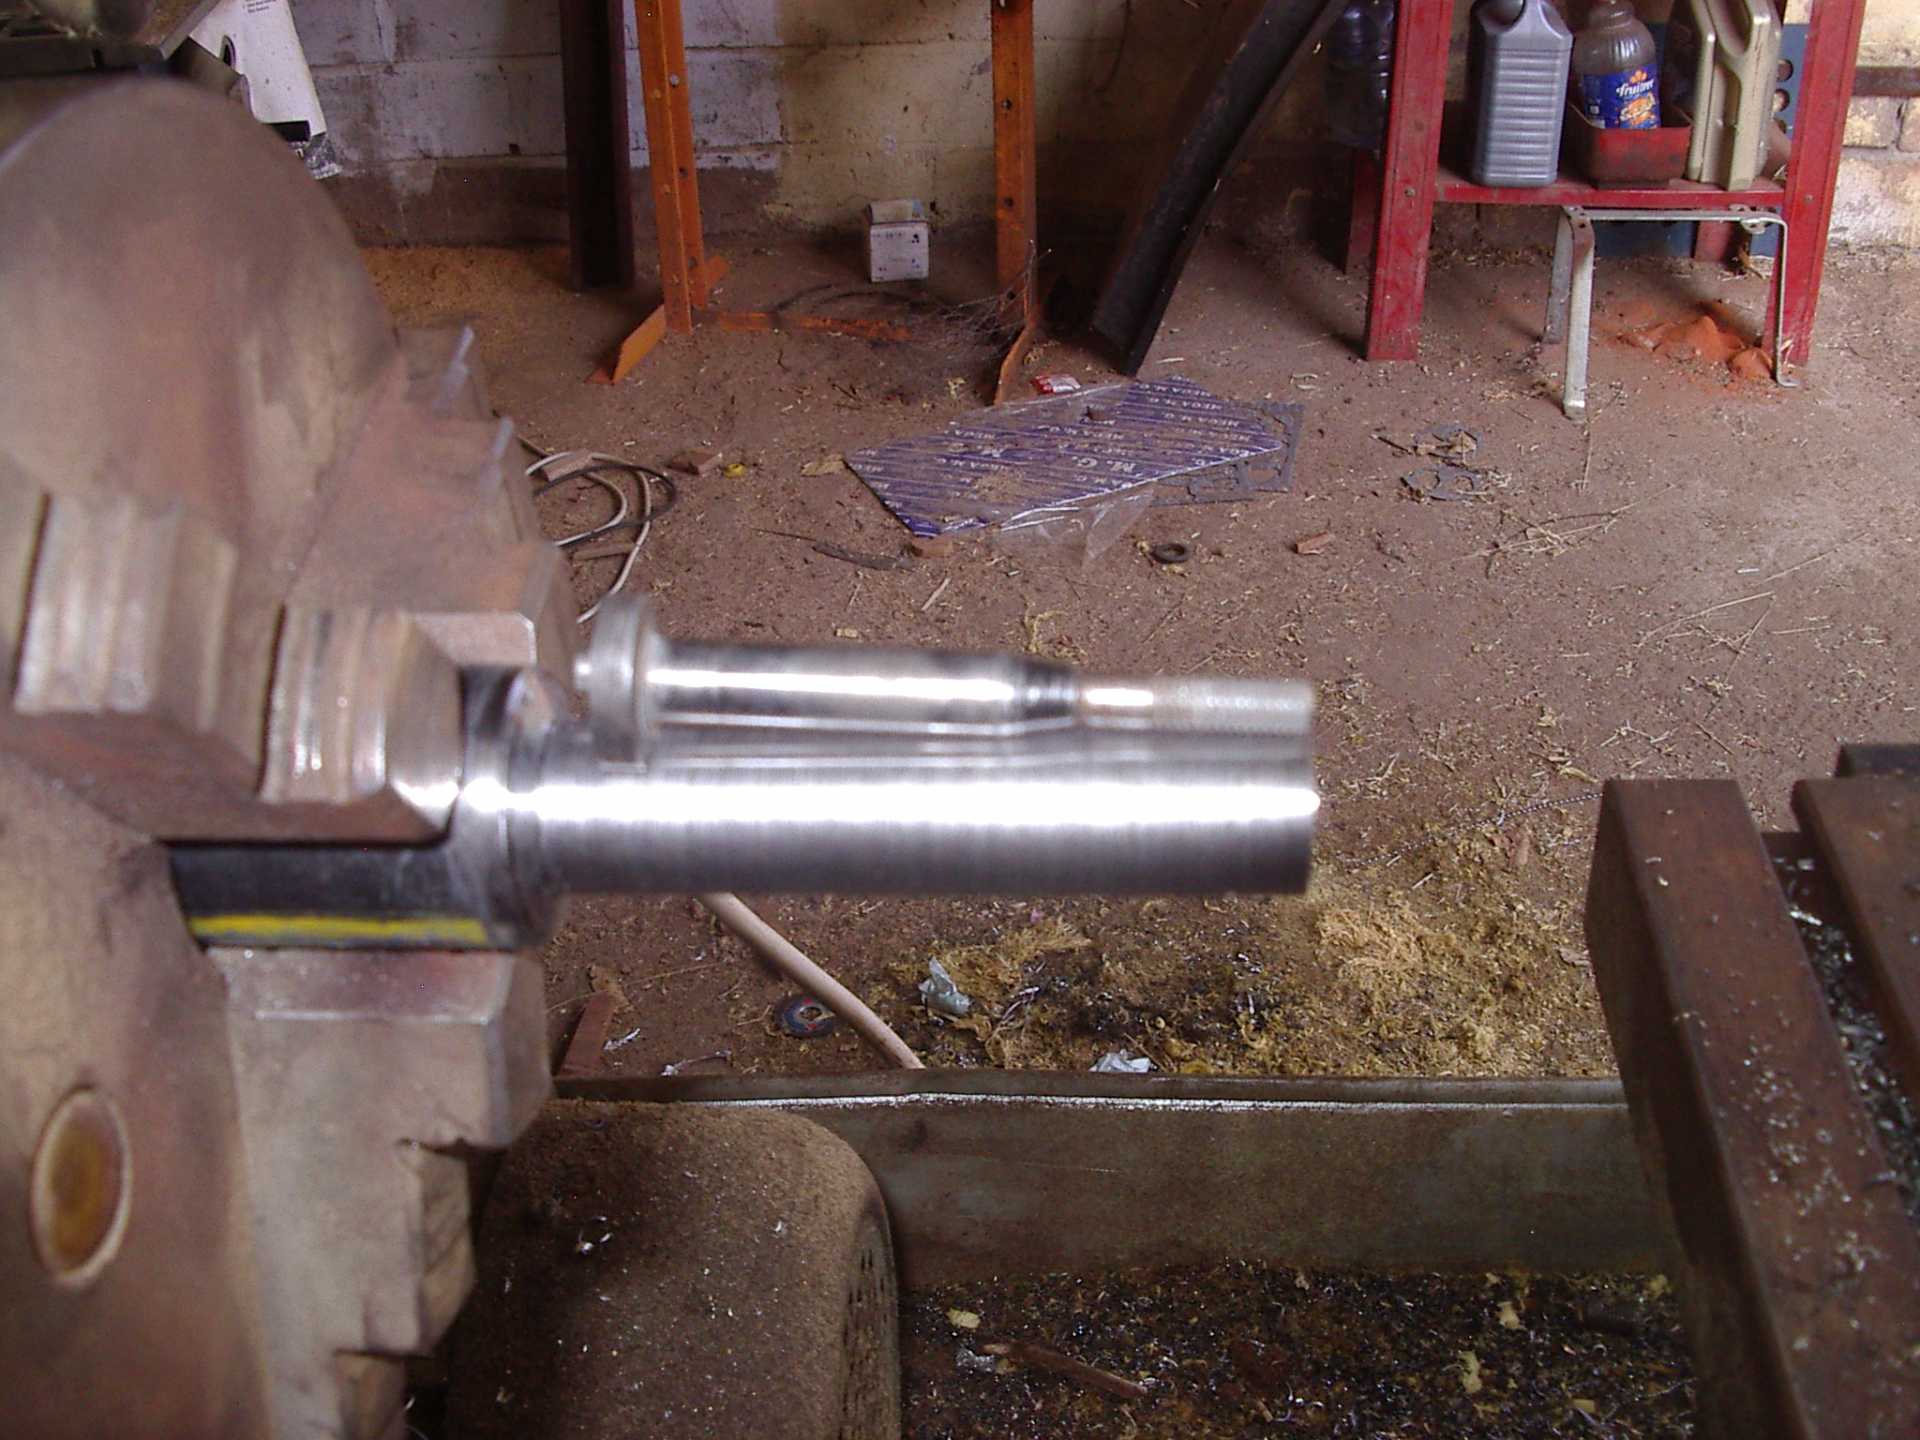
Then down to shaft size, plus a bit.

I've left about .2mm (8thou), I hope this will be enough for lapping.
Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.
- Klipkopwildlife
-
Topic Author
- Offline
- Administrator
-
- I'm supposed to be retired!

I will then thread the end 2BA while I still have the advantage of the thicker shaft.

I always make a drawing for posterity, my Engineering master at school would have had a fit! But at least I know what it looks like!
Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.
- Klipkopwildlife
-
Topic Author
- Offline
- Administrator
-
- I'm supposed to be retired!
The manufacturers intended to have all surfaces glass hard to reduce friction and enhance life, personally I don't think they've gone the right way about it, and certainly the reviewer in the article was not overly impressed. He battled to get one engine to run consistently and the other took a long time to approach consistency and higher revs. It got so hot he had to pour raw fuel over the crankcase to cool it down!
A brief word about terminology, hard is not necessarily strong, tough is not necessarily hard. Hard and tough together is good, today we can surface harden a tough material using a coil driven at high frequency. When we pass a shaft through the coil the surface heats up and we then quench immediately using a ring of fluid jets. This gives us the best of both worlds, a glass hard outer with a tough inner as support. We can even control the degree and depth of hardness by adjusting frequency, current, speed of pass, and type of fluid used for quenching.
If we want to get really fancy we now have steels that must be heated in an oven containing an inert (specific) gas and held within 5o of a specific temperature for a specific length of time Using todays methods we could make model engines that will literally last for ever, running on a breath of oil, or no oil in the case of a petrol engine. The only problem would be, we couldn't afford them!
Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.
- Quorneng
-
- Offline
- Forum Master
-
- Posts: 10058
- Thank you received: 19043
'case hardening' is a viable option where the part (and it can be in its finished state!) is heated and submerged into a bed of carbon rich material. The carbon locally migrates into the low carbon steel raising its carbon content. When quenched it produces a 'glass hard' skin of high carbon steel without altering the properties of the majority of the base material.With care it is possible to case harden just the bearing surfaces of a crankshaft leaving the rest in its tough/strong condition.
I believe this is what was done on the original Mills 75 where the threaded nose of the hard crankshaft would bend and could safely be straightened again.
Mine did and has been!

Please Log in or Create an account to join the conversation.
- Klipkopwildlife
-
Topic Author
- Offline
- Administrator
-
- I'm supposed to be retired!
I don't know how this material will react to heating and quenching, at the moment after finish lapping it's .03mm larger than the sample, any 'pull' in the structure will mean it will no longer fit.To continue, threading after first checking the thread is correct.
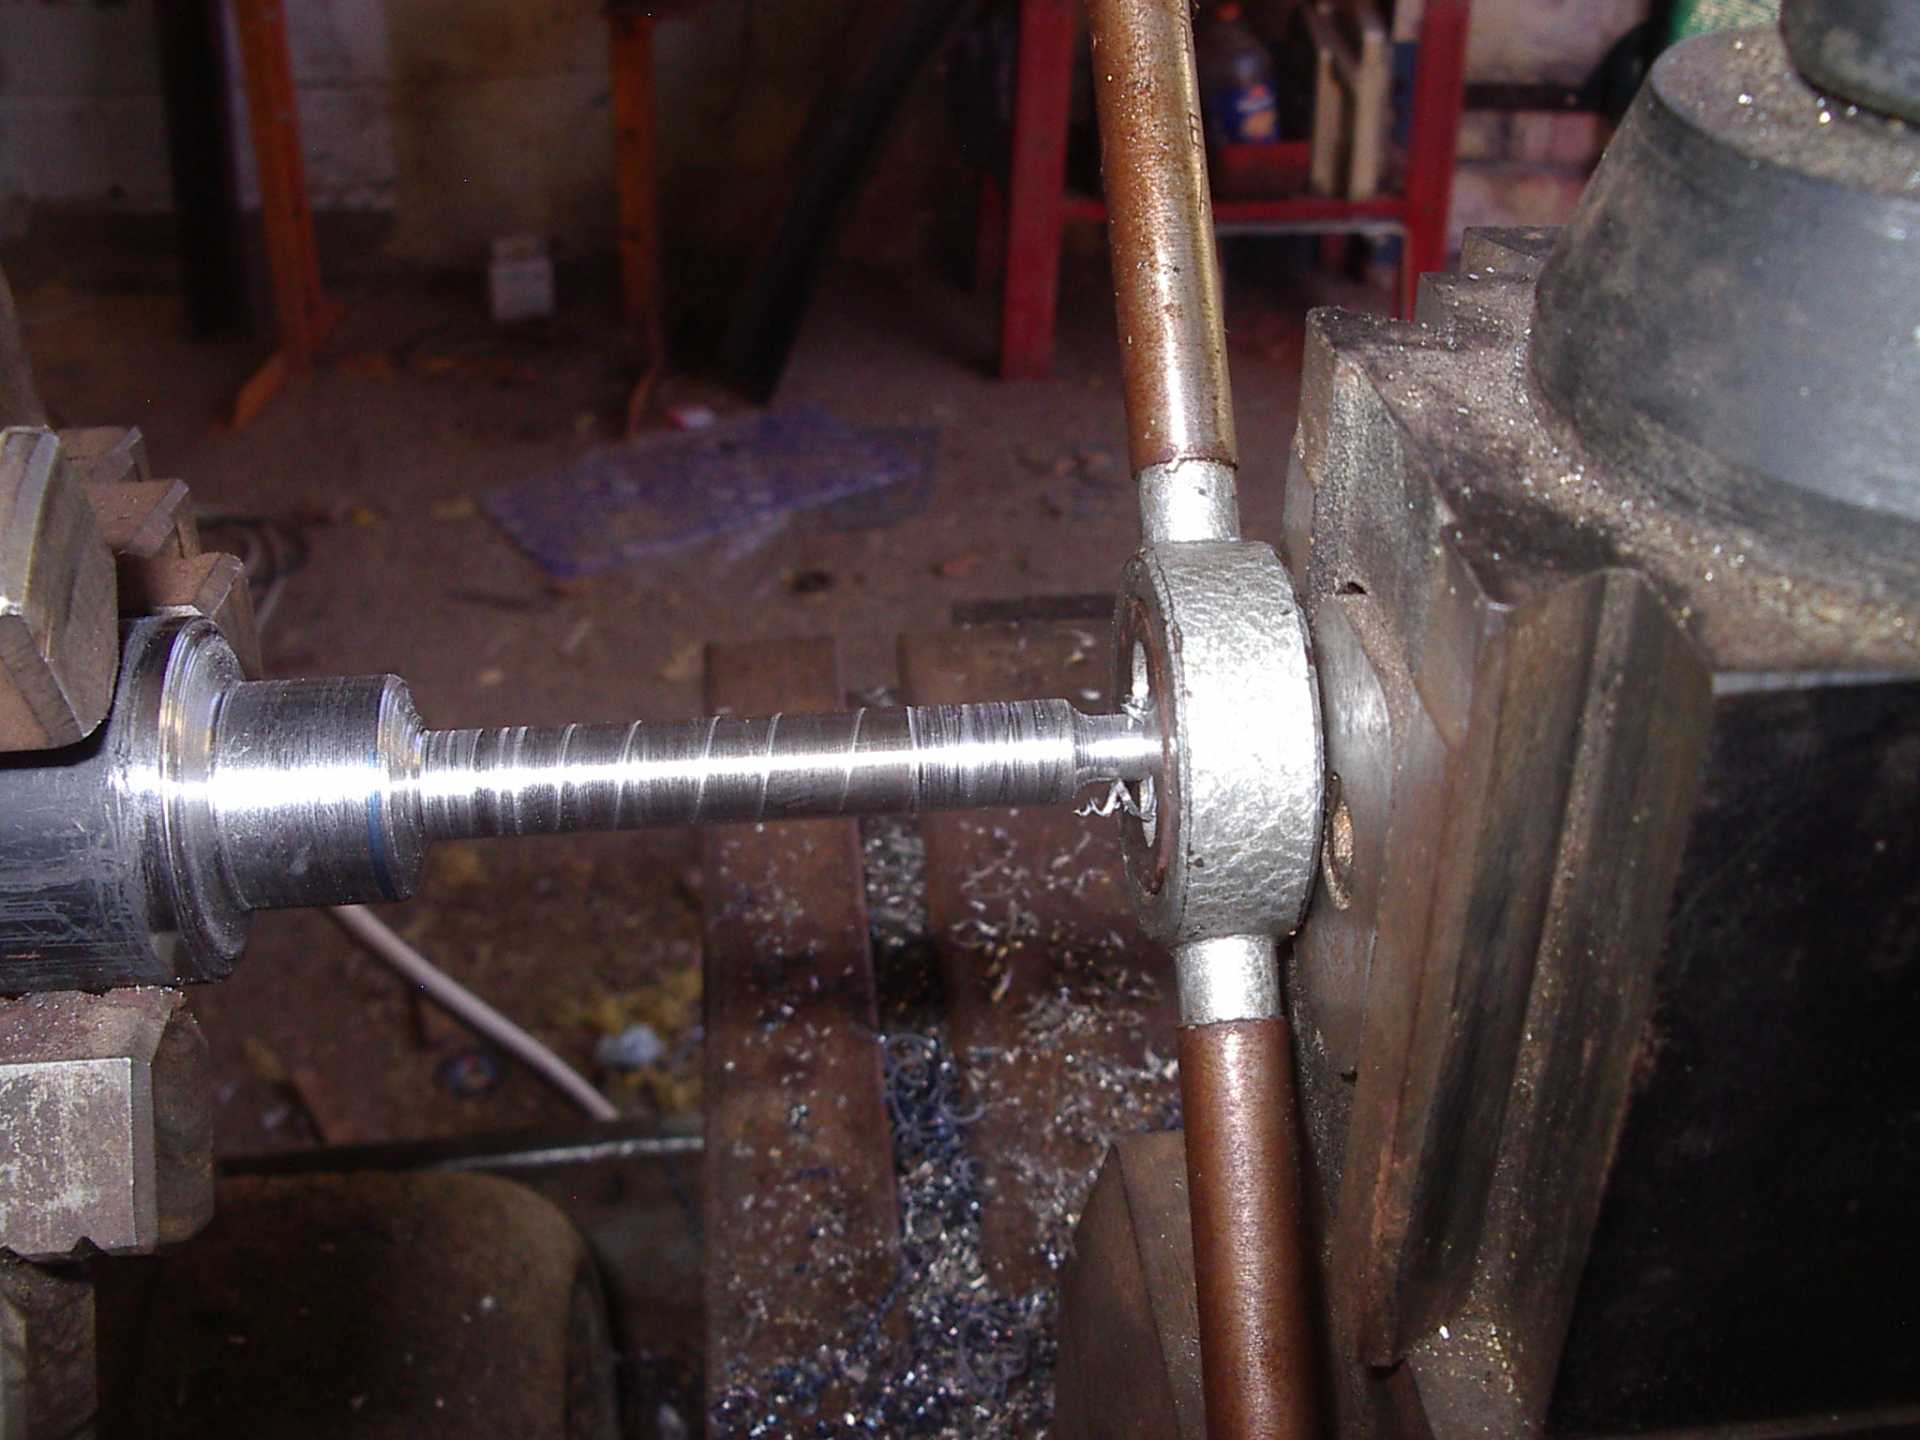
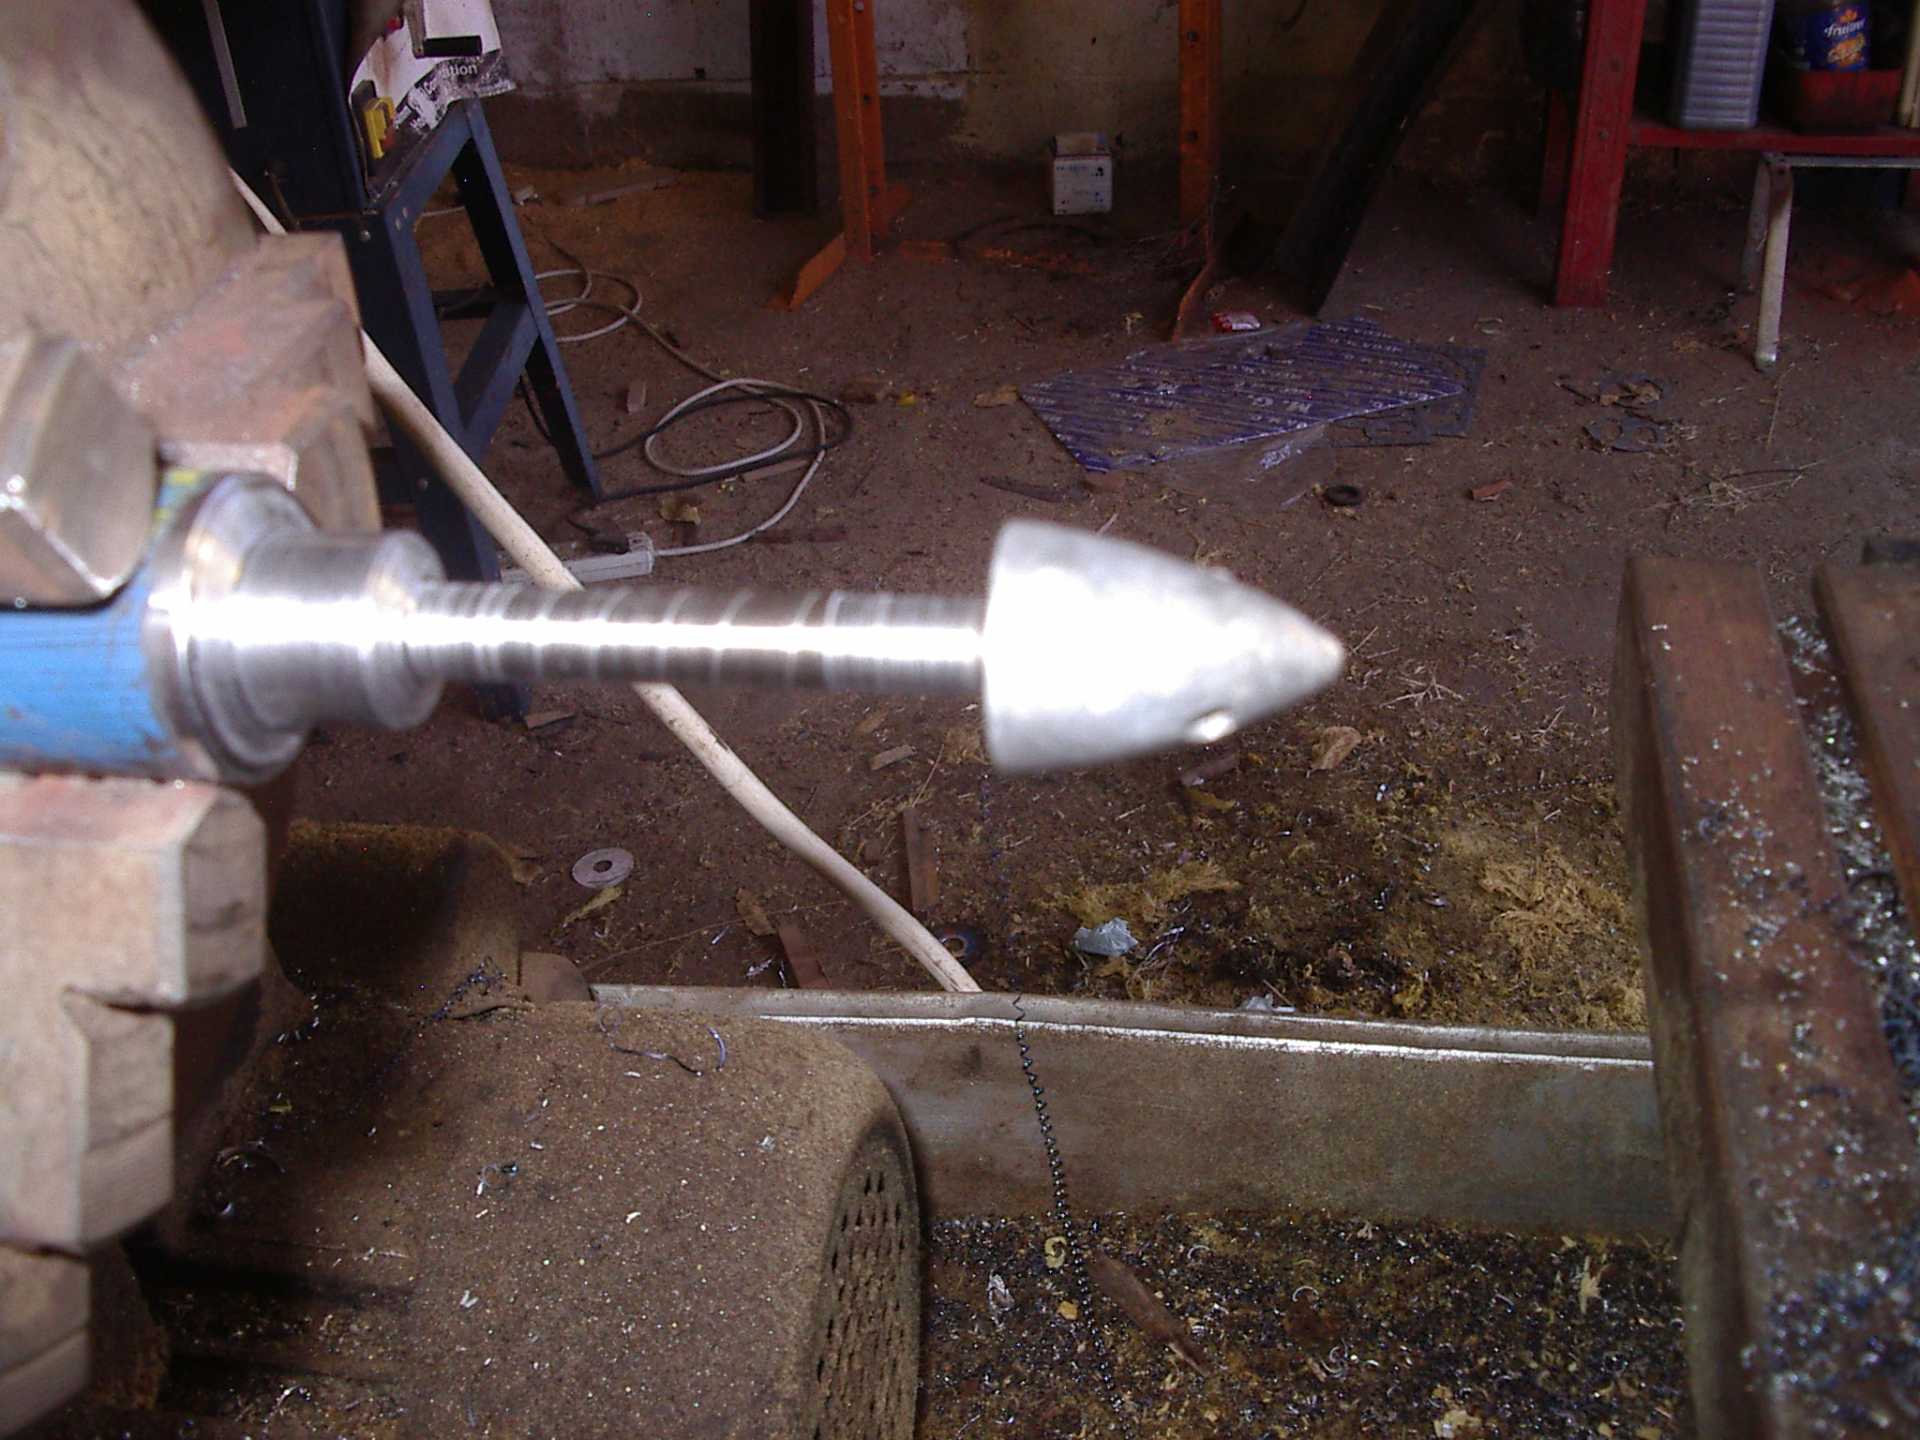
finish lapped with the driver taper machined.

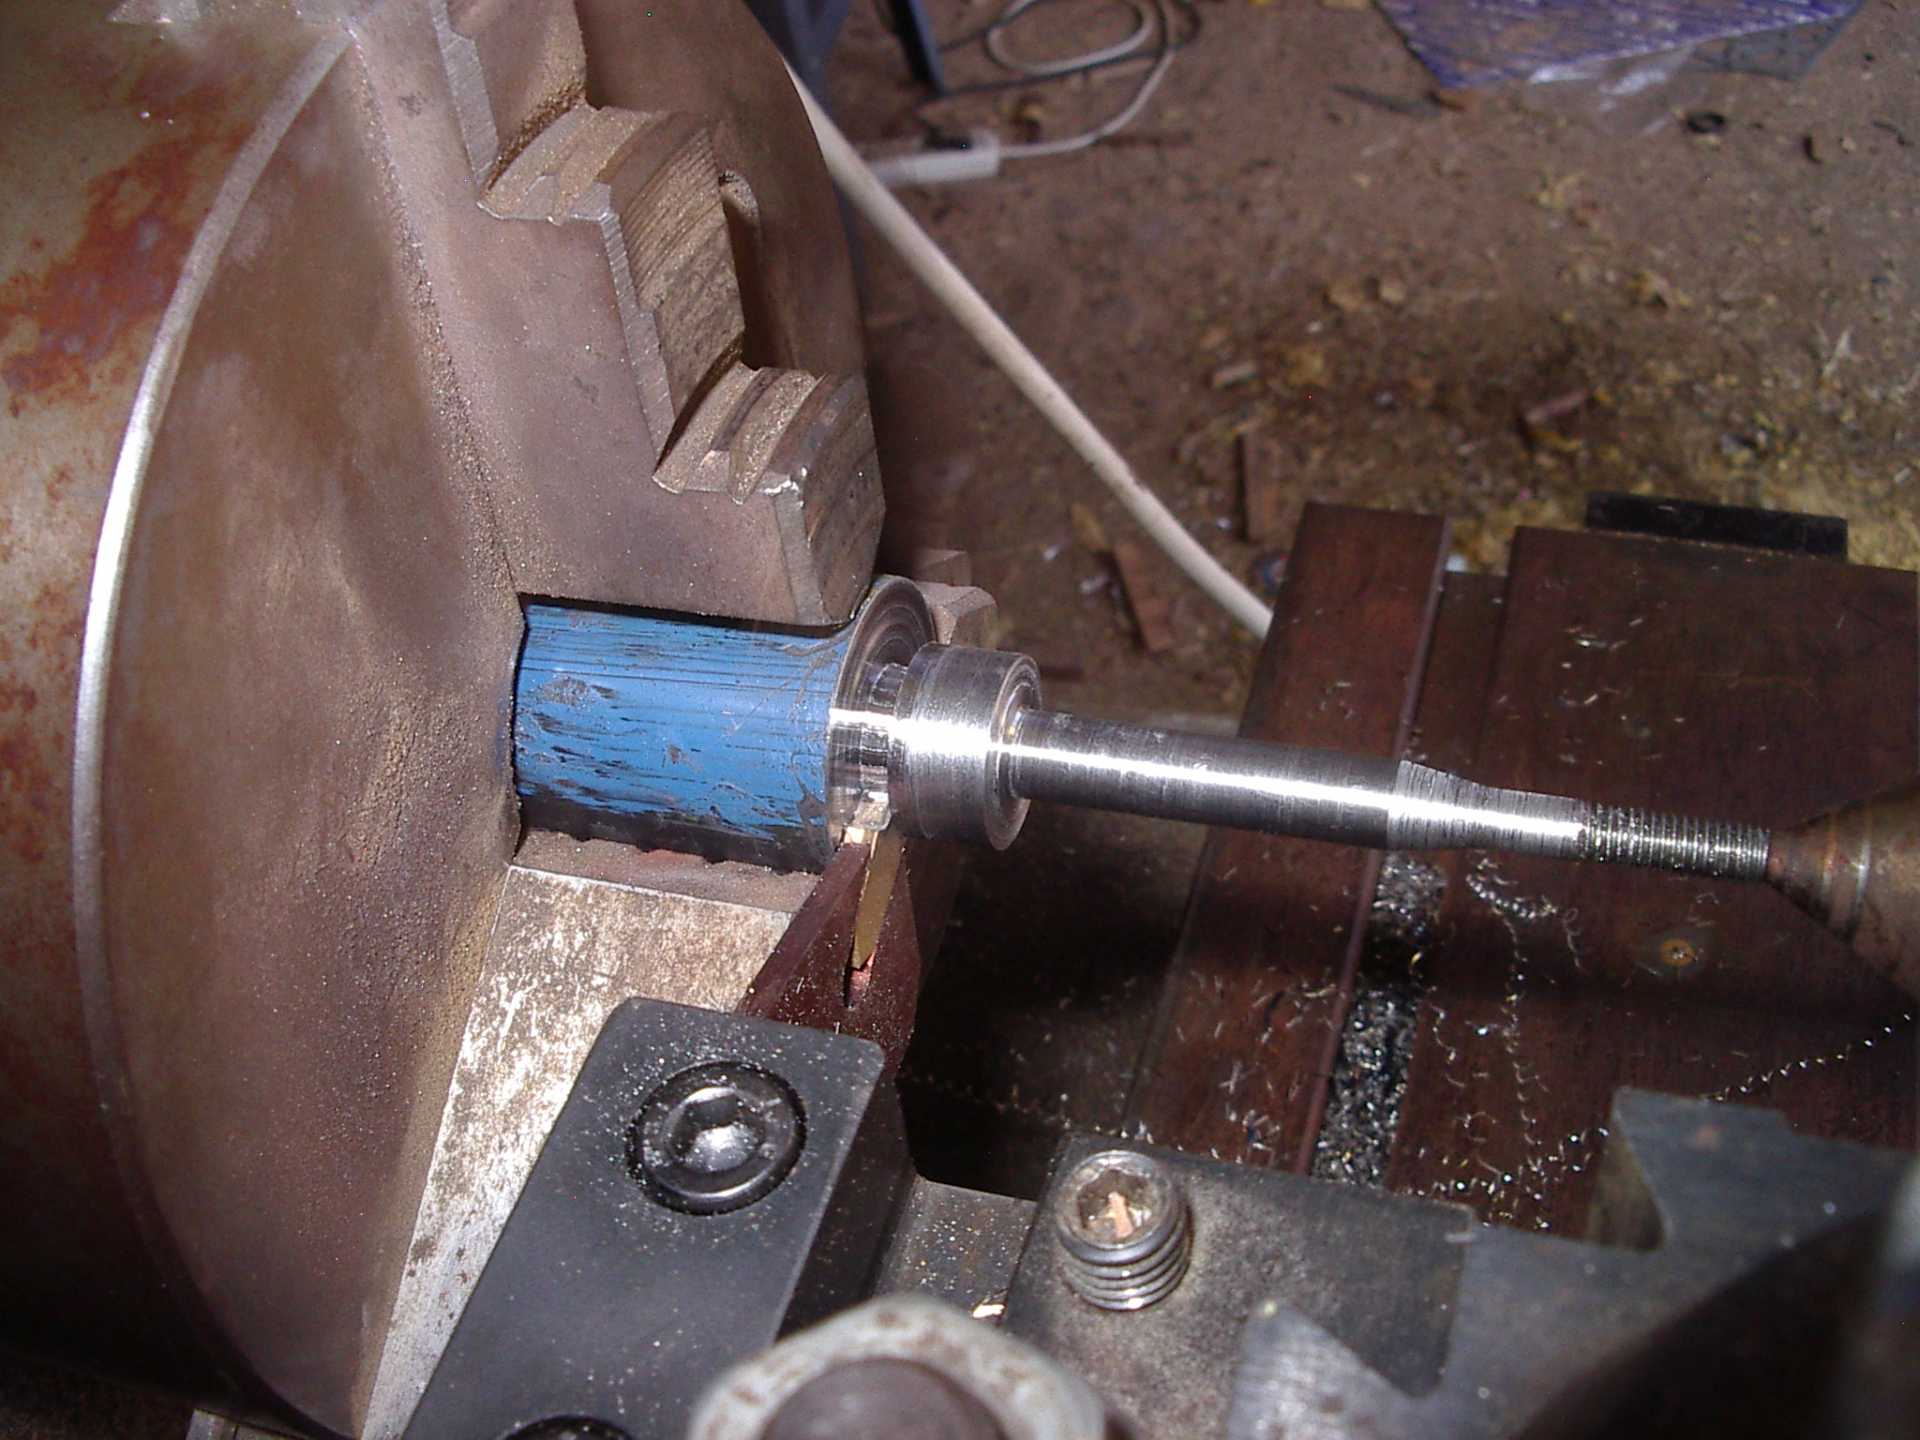
and ready to part off, not a job I enjoy, it needs a really rigid machine because the tip is so wide at 3mm
Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.
- one tenor
-

- Offline
- Forum Veteran
-

- johnpcalex@gmail.com
Anything will fly given enough power
Please Log in or Create an account to join the conversation.
- Klipkopwildlife
-
Topic Author
- Offline
- Administrator
-
- I'm supposed to be retired!

And with the shaft blank in place.

And make sure it's running true.
Do it now, you may never get another chance
Please Log in or Create an account to join the conversation.
- one tenor
-
- Offline
- Forum Veteran
-
- johnpcalex@gmail.com
 Nice kit Klip.What next? Just thinking if I did case harden the shaft and it grew /stretched I could lap the bore in the crankcase CAREFULLY for best fit.
Anything will fly given enough power
Please Log in or Create an account to join the conversation.
- THE BLACKBIRD
-

- Offline
- Forum Master
-
- Posts: 6781
- Thank you received: 10722

Please Log in or Create an account to join the conversation.
- one tenor
-
- Offline
- Forum Veteran
-
- johnpcalex@gmail.com
Nice kit Klip.What next? Just thinking if I did case harden the shaft and it grew /stretched I could lap the bore in the crankcase CAREFULLY for best fit.BTW you said something about the power of your lathe not up to some work, a bit ago.Apart from fitting a more powerful motor you could try a new belt. As belts wear there comes a time when even as tight as you can get them they slip because the vee has worn down and the only friction area is the tip of the Vee. A new belt can sometimes work wonders. One of the toothed ones may help. If granny has already sucked this egg I apologise . I remember one C/H pump I was looking at in a presbytery .The priest in charge was saying how the noise from it kept them all awake. I slackened the belt and spun the motor and pump and there was no sound from either . I then gave the belt a twist and revealed loads of cracks. In fact it was all cracks. I found a suitable car belt .Fitted it and Silence. The difference was astounding. The priest was very grateful as their plumber said they needed both replaced.Robbing bleeder..Anyway it might be worth a try.

Anything will fly given enough power
Please Log in or Create an account to join the conversation.
- one tenor
-
- Offline
- Forum Veteran
-
- johnpcalex@gmail.com
